Product · Rotary motion
Gear Shafts
Integral gear shafts, spline shafts, motor shafts, and stepped shafts — built to your drawing.
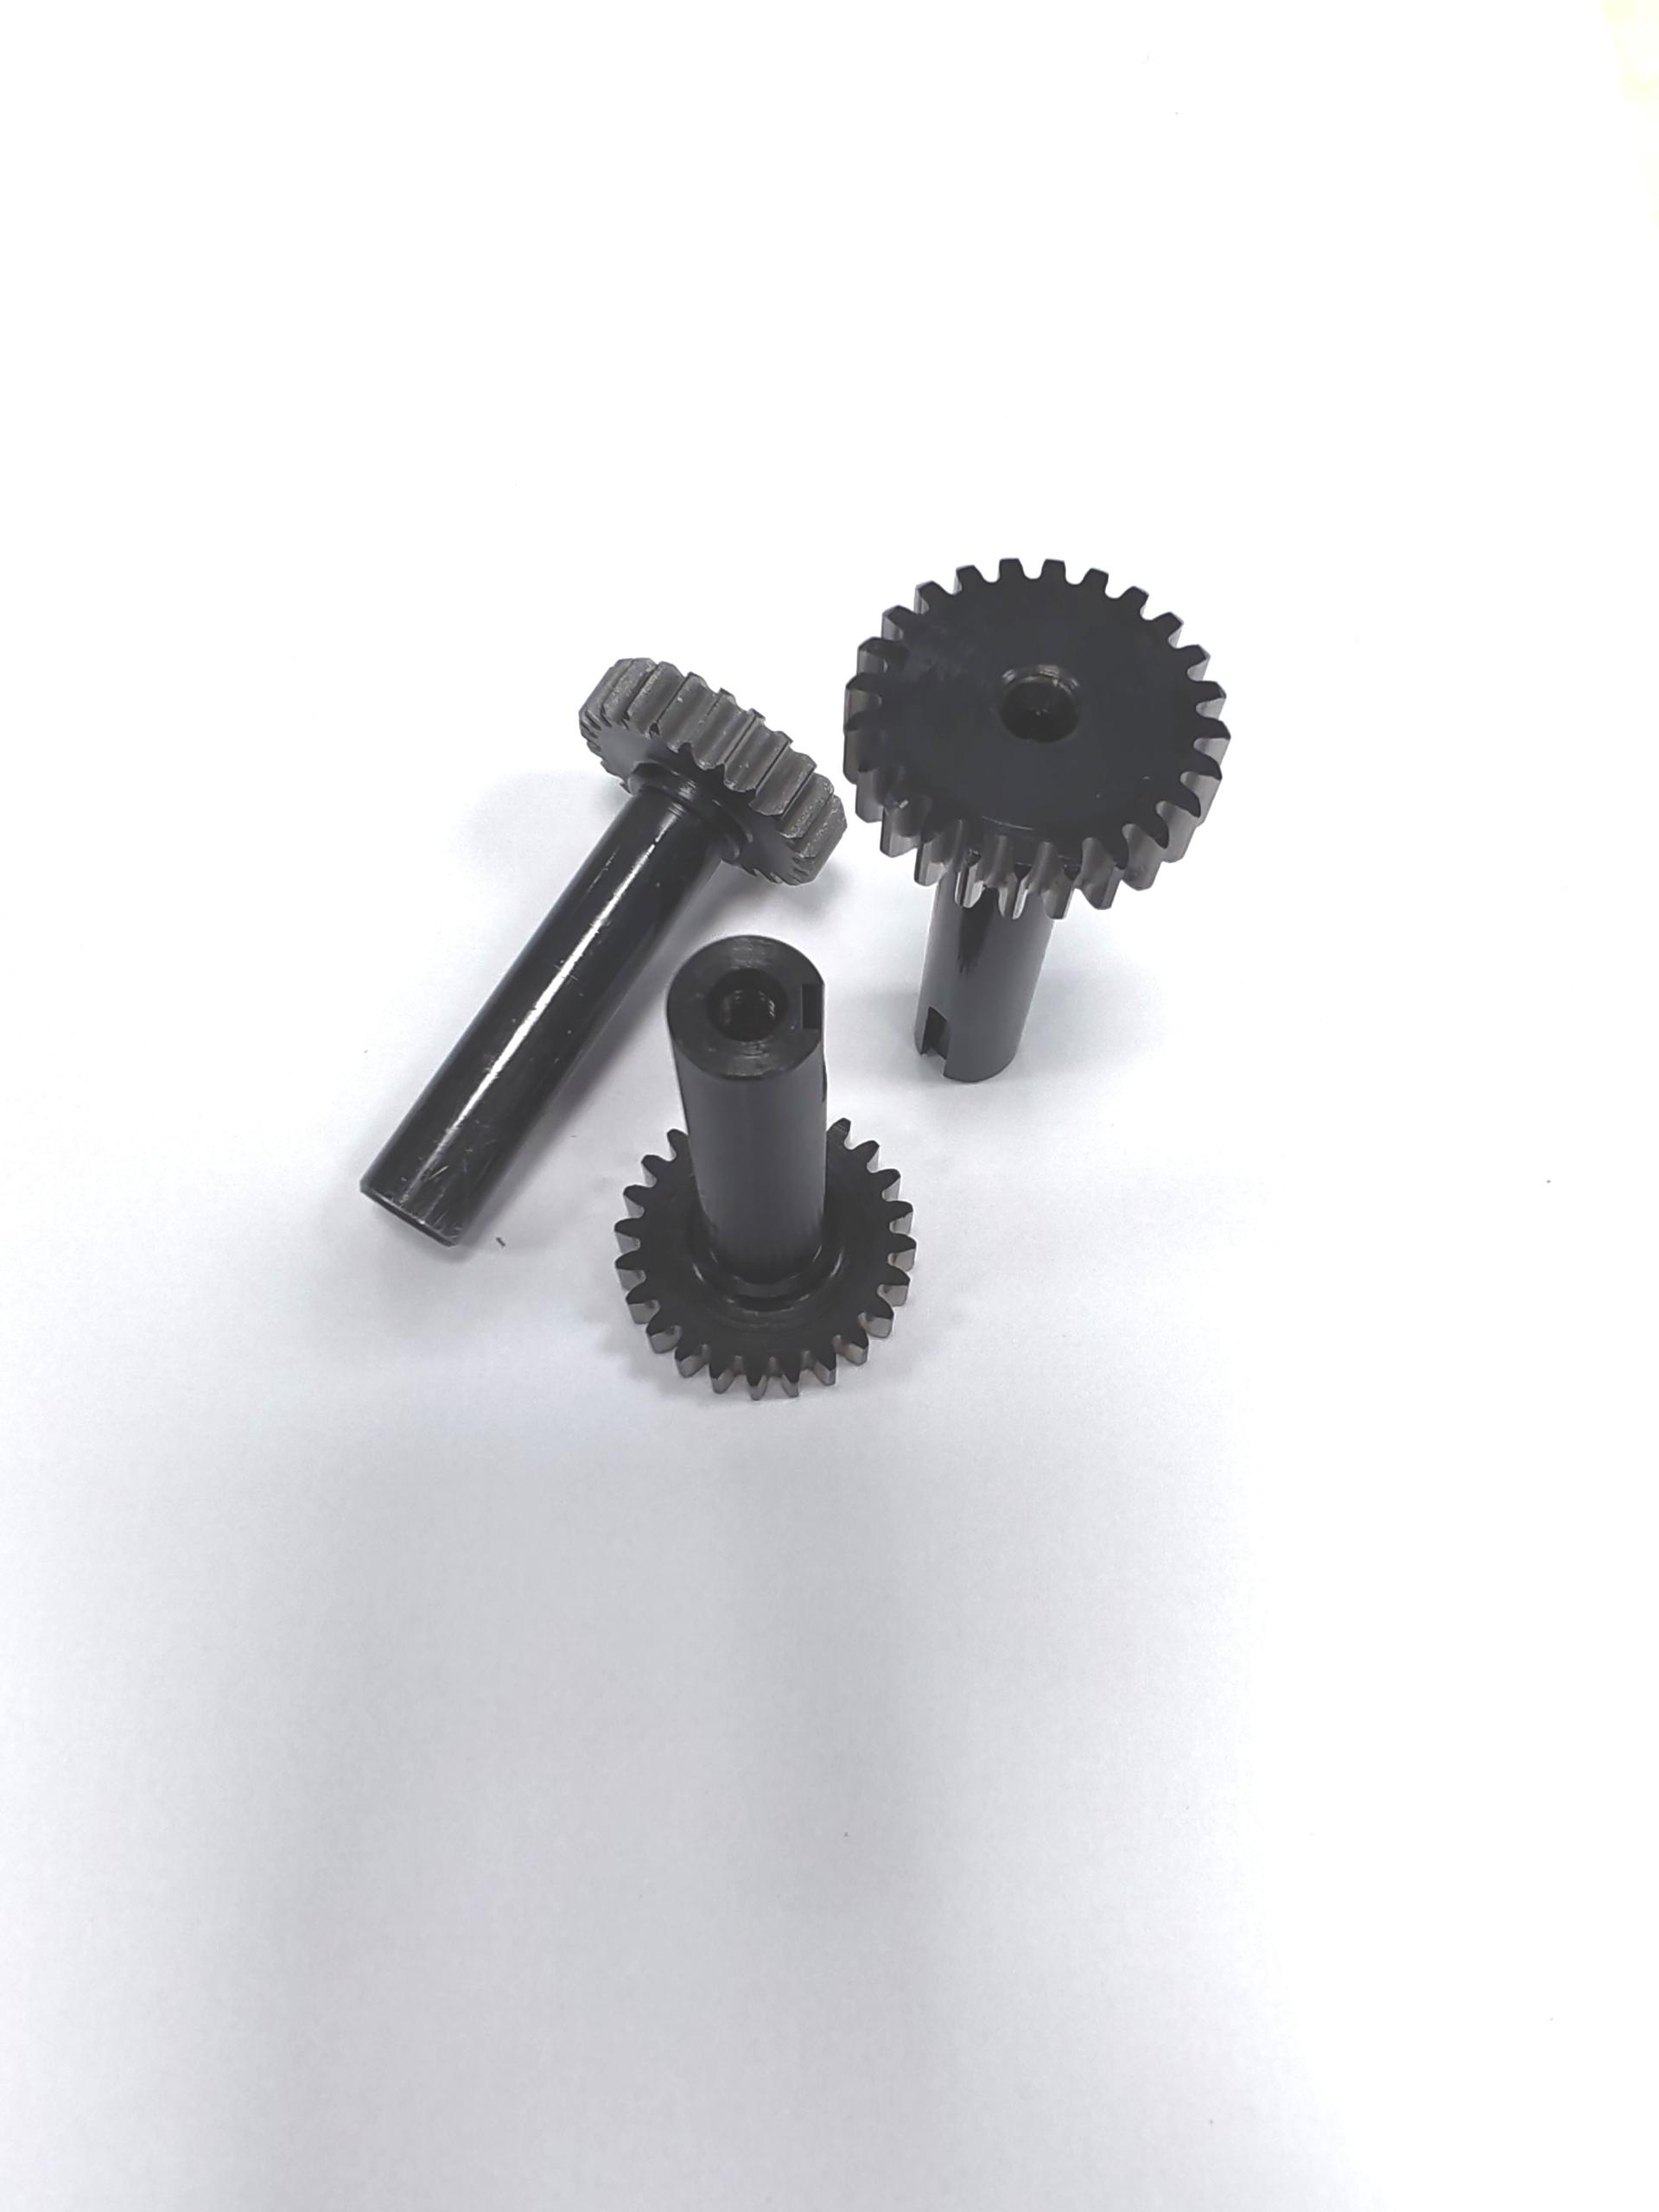
When a gear is cut directly onto the shaft body, you eliminate a keyed joint, an interference fit, and a runout stack-up. Wolfer manufactures integral gear shafts — and the related families of spline, motor, and stepped shafts — from quenched-and-tempered or case-hardened steels, ground after heat treatment.
Last updated Reviewed by Luo Genwen, Production Plant Manager
-
Length
Up to 1,500 mm
-
Diameter
Ø8 – Ø200 mm
-
Runout
≤ 0.01 mm (ground)
-
Hardness
HRC 28–62 depending on heat treat
What we make
Gear Shafts we cut from drawings.
One-Piece Gear Shafts
One or more gear sections cut directly into the shaft body
Spline shaft
Involute (ISO 4156 / ANSI B92.1) or straight-sided (DIN 5462 / 5463) splines
Motor shaft
Custom motor shaft extensions, with encoder bores and keyways
Ball-screw end machining
Ball-screw shaft ends machined to your drawing
Stepped shaft
Multi-diameter shafts for bearing stack-ups
A "gear shaft" can mean three different things to three different engineers — Wolfer covers all three. (a) Integral gear shaft: a gear cut into the shaft body, no key joint. (b) Spline shaft: standard or custom involute / parallel-key splines. (c) Stepped / motor shaft: turned, ground, and balanced to fit a specific motor frame.
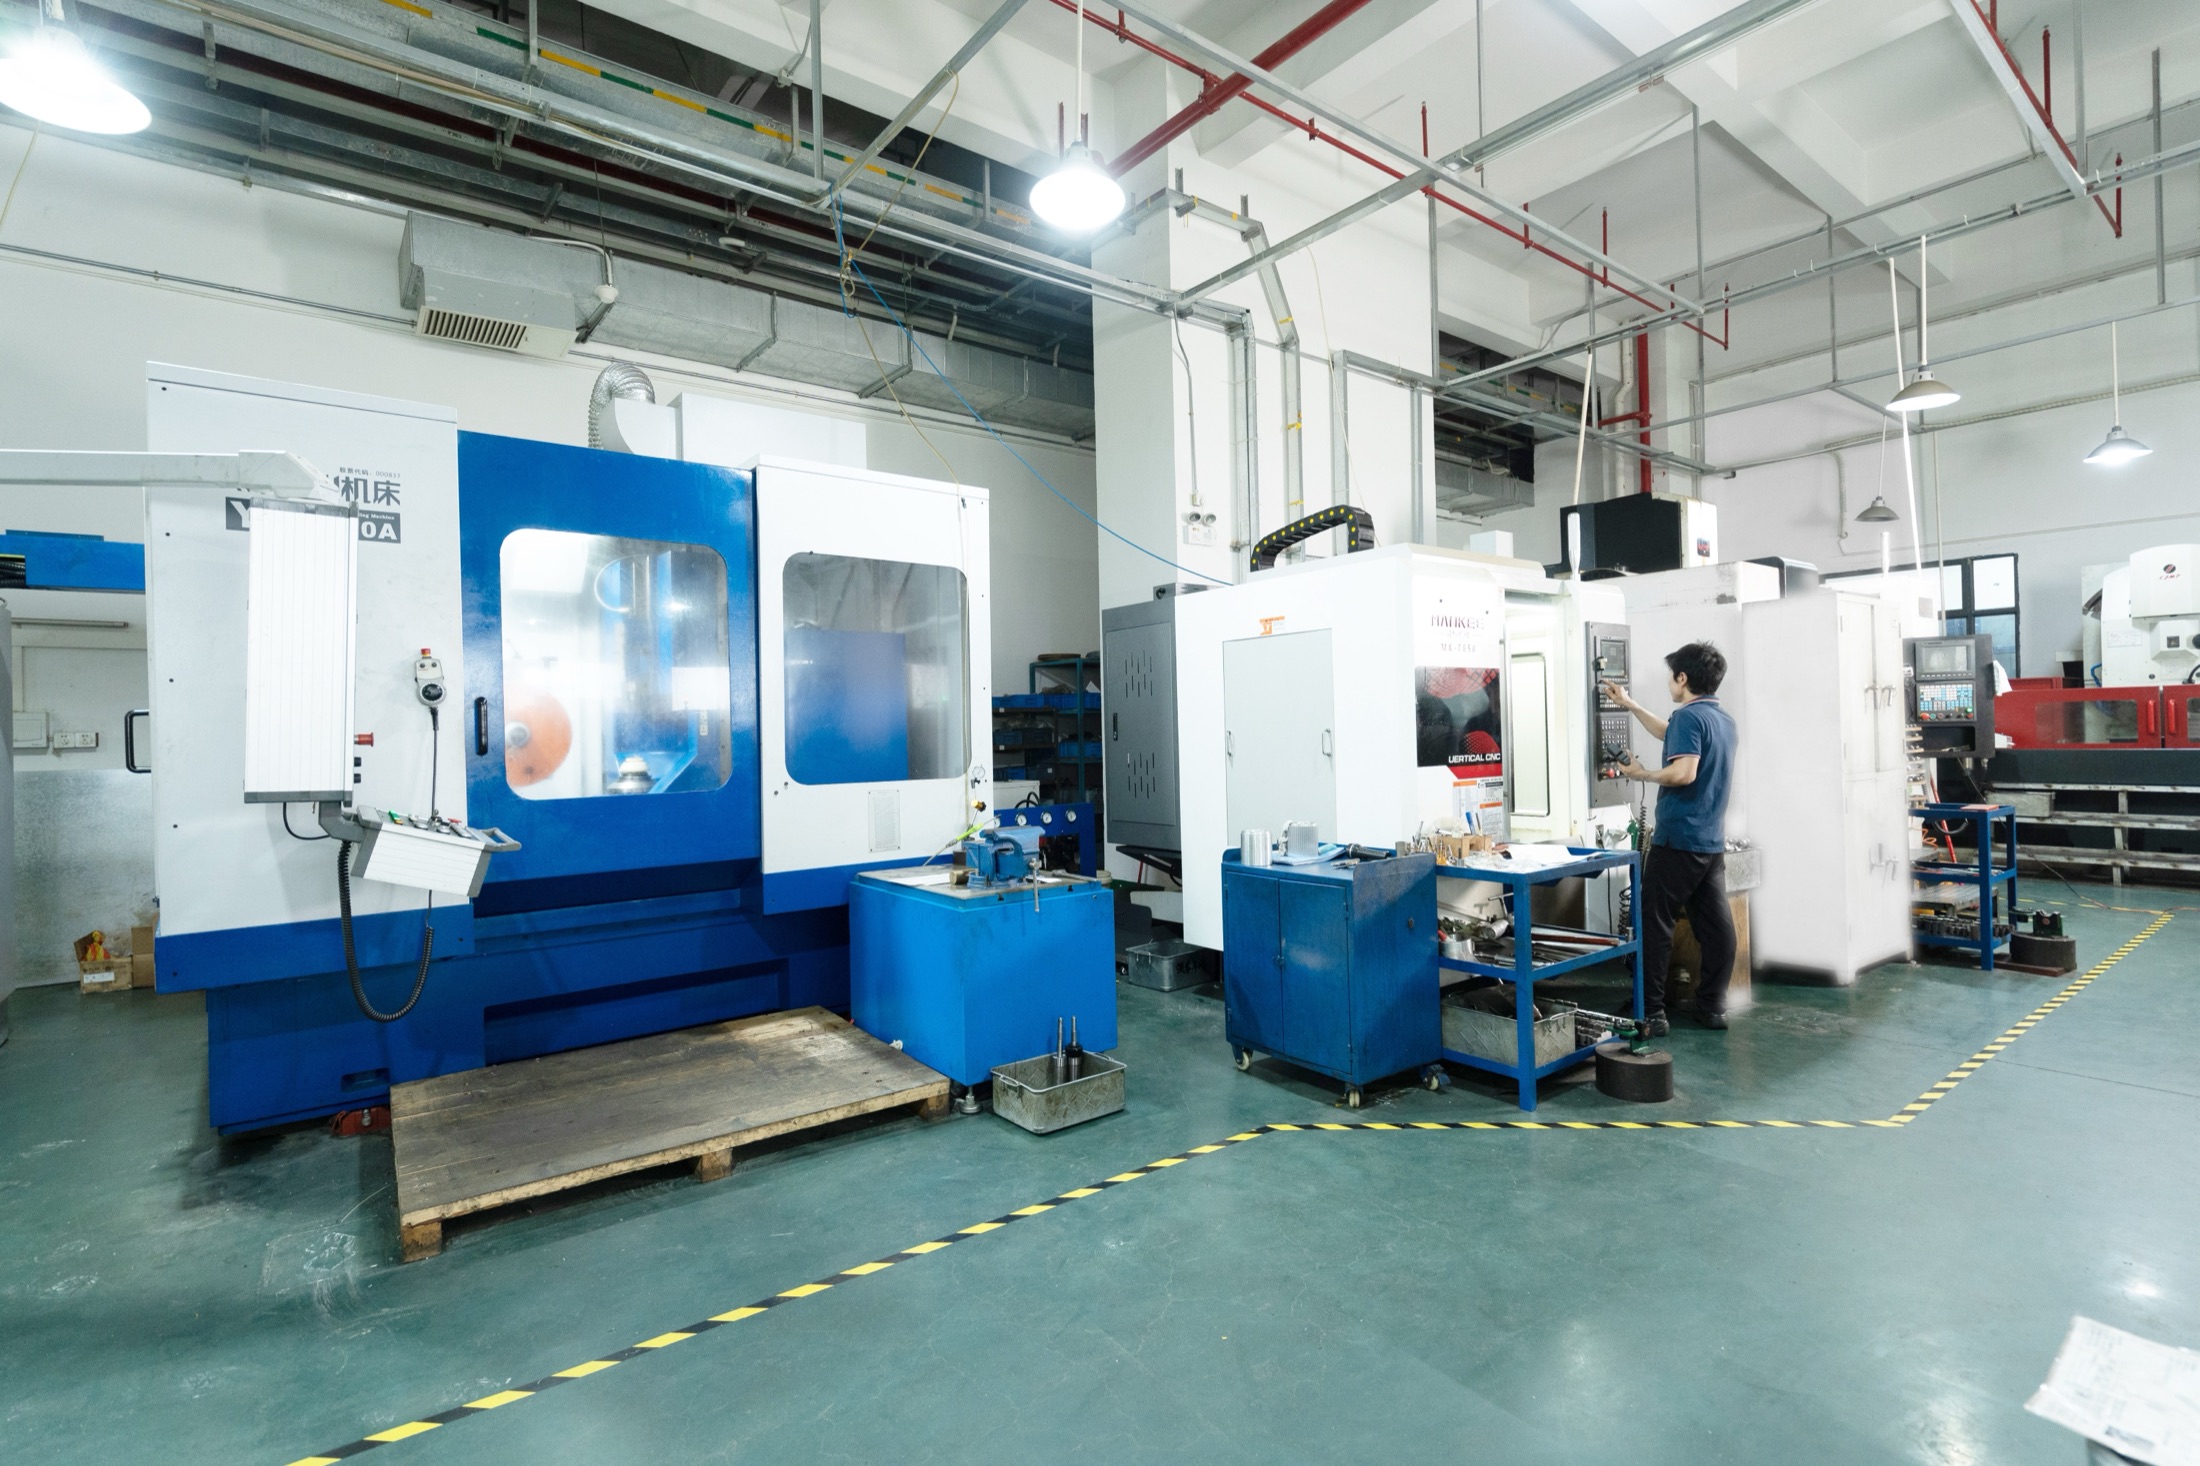
Critical surfaces (bearing journals, gear pitch diameter, spline major / minor diameter) are ground after heat treatment. Total indicated runout (TIR) on bearing journals is typically held to ≤ 0.01 mm (0.0004 in). Surface roughness on ground journals is Ra 0.4 µm (16 µin).
We balance long shafts on a two-plane dynamic balancer when the customer drawing calls for it — typical balance grade G2.5 per ISO 1940.
Standards
Built to international tolerance specs.
- ISO 4156 (involute spline)
- DIN 5462 / 5463 (parallel spline)
- ISO 1940 (dynamic balance)
Inspection
Every part measured before it ships.
- Between-centers runout check on precision bench centers
- CMM — concentricity of gear pitch-diameter to bearing journals
- Dynamic balancing machine (Haimer / Tonsong)
- Surface roughness tester
Applications
Where these parts go to work.
FAQ
Common questions from engineers buying this product.
Why choose an integral gear shaft over a separate keyed gear?
Two reasons: backlash and runout stack. An integral gear has no keyway clearance, so backlash is determined only by tooth-flank tolerance. And the gear pitch diameter is cut concentric to the same centers as the bearing journals, so total runout is the lowest you can get without a flange-mount bearing.
Can you supply a shaft with two different gear modules?
Yes — we routinely make double-gear shafts where the input pinion is m 1.5 and the output pinion is m 3. Both sections are hobbed and ground after heat treatment in the same setup.
Related products
Often quoted together.
Gears
Custom precision gears, built from your drawings — spur, helical, bevel, worm, and internal.
View product →Couplings
Rigid and flexible shaft couplings — including jaw couplings, beam (helical-slit) couplings, diaphragm couplings, disc couplings, bellows couplings, and Oldham couplings — all built to drawing.
View product →Machined Transmission Parts
CNC-turned and milled non-standard transmission components, from your DWG or STEP file.
View product →Ready to start your gear shafts project?
24-hour quote · engineering review within one business day · ≤ 30 days to ship after approval.